

Why Continuous Differential Pressure Monitoring Is Critical in Pharmaceutical Cleanrooms
A pharmaceutical cleanroom’s pressure cascade does a critical job: keeping air and everything carried in it moving away from your most sensitive areas. Continuous environmental monitoring gives you documented proof…

A pharmaceutical cleanroom’s pressure cascade does a critical job: keeping air and everything carried in it moving away from your most sensitive areas. Continuous environmental monitoring gives you documented proof that it’s working across every batch period and audit window, but only if the system is designed and installed correctly.
A well-designed cleanroom differential pressure monitoring program comes down to three things:
- How sensors are placed
- How your cleanroom monitoring system is configured
- How easy the data is to trace and verify in an audit
Here’s what each of those looks like in practice.
Best Practices for Cleanroom Monitoring Systems
Here’s what a well-designed cleanroom differential pressure program does right:
- Sensor Placement
Sensor placement determines whether your differential pressure data is accurate and whether your deviation record is defensible. Two placement decisions determine whether that sensor produces reliable data:
Zone boundary coverage. Each zone boundary — Grade B to Grade C, Grade C to Grade D — needs its own dedicated sensor. A single sensor covering multiple zones can’t tell you which boundary failed, when, or by how much.
Position within that boundary. Locate sensors at the actual differential pressure boundary between adjacent areas, away from supply air diffusers, doors, and high-traffic zones. Industry guidance recommends placing reference measurement points in a protected technical area or in the space between the cleanroom and building exterior, shielded from door events and external differential pressure fluctuations.
- Cleanroom Monitoring System Configuration
Alarm delay configuration is one of the most consequential decisions in a differential pressure monitoring program. It is also one of the most frequently overlooked. Two failure modes are equally common:
Delays set too short trigger an alarm on every door opening, producing alert fatigue that leads staff to override notifications and miss genuine failures.
Delays set too long allow real differential pressure failures to go undetected before they affect product quality or generate a deviation.
The right parameters come from your risk assessment and should be validated as part of your monitoring qualification specific to your facility’s door frequency, zone criticality, and validated operating ranges.
- Data Traceability
When a differential pressure excursion occurs, correlating it with temperature and door activity is what turns a deviation record into an actual explanation. Two scenarios consistently create traceability gaps:
Differential Pressure data in a standalone system. If differential pressure records can’t be viewed alongside temperature monitoring, humidity monitoring, and door open/close data from the same window, deviation investigations require manual reconciliation across disconnected sources, introducing delay and error risk.
Differential Pressure data in a building management system not integrated with your EMS. A BMS captures differential pressure readings but typically doesn’t produce the time-synchronized, audit-trail-capable record a GxP inspection requires. When a regulator asks for the environmental record for a specific batch period, the answer should come from one system.
What the Regulatory Frameworks Require
Across every major framework governing pharmaceutical cleanrooms, the expectation is consistent: pressure differentials must be defined, continuously monitored in critical areas, and documented in a system that produces retrievable, audit-trail-capable records. Here’s what that looks like from a regulatory perspective:
International Standardization for Organization (ISO) 14644-2 requires a documented, risk-based monitoring plan that demonstrates ongoing environmental control between certification cycles. For facilities where differential pressure is a critical parameter, that plan must address continuous monitoring, not just periodic verification.
ISO 14644-4 addresses pressure differential requirements in cleanroom design, establishing the engineering basis that monitoring programs are built on.
Food and Drug Administration (FDA) 21 CFR Parts 210 and 211 require documented environmental control in U.S. pharmaceutical manufacturing areas, with electronic records meeting 21 CFR Part 11 requirements for data integrity, audit trails, and access controls.
United States Pharmacopeia (USP) <797> addresses airflow and pressure differential relationships in sterile compounding areas. It requires that ISO Class 5 primary engineering controls operate within a positive pressure environment, and that pressure differential relationships between compounding areas and adjacent spaces be documented as part of ongoing environmental monitoring — not just verified at initial certification.
USP <800> requires documented negative pressure for hazardous drug compounding rooms relative to adjacent spaces. That documentation obligation extends beyond the physical pressure differential itself. It includes the alarm response record, the deviation investigation, and evidence that the negative pressure was maintained continuously across the compounding period, not just at the start of each shift.
How DicksonOne Fits Into Your Cleanroom Monitoring Program
Unlike other environmental monitoring systems, DicksonOne doesn’t require you to replace existing infrastructure. Dickson’s Cobalt X data logger accepts a universal 4-20 mA input, capturing output from already-installed differential pressure transmitters alongside temperature, humidity, CO₂, and door open/close data — all in one audit-trail-capable platform.
Here’s what that means for your monitoring program:
Your differential pressure data is no longer isolated. All environmental parameters (differential pressure, temperature, humidity, CO₂, and door open/close) are time-synchronized in one system, so deviation investigations and batch documentation draw from a single, coherent record.
Your audit trail is built in. Dickson’s systems export reports with complete access logs, alarm acknowledgment records, and calibration history, meeting audit requirements without manual data assembly.
Your compliance program runs on one validation. One platform, one set of access controls, one calibration schedule. This reduces the administrative overhead of maintaining a standalone differential pressure monitoring system alongside your other environmental parameters.
If your cleanroom differential pressure monitoring isn’t producing audit-trail-capable records alongside your temperature and humidity data, talk to a Dickson expert about making sure that a complete record exists and is ready when you need it.
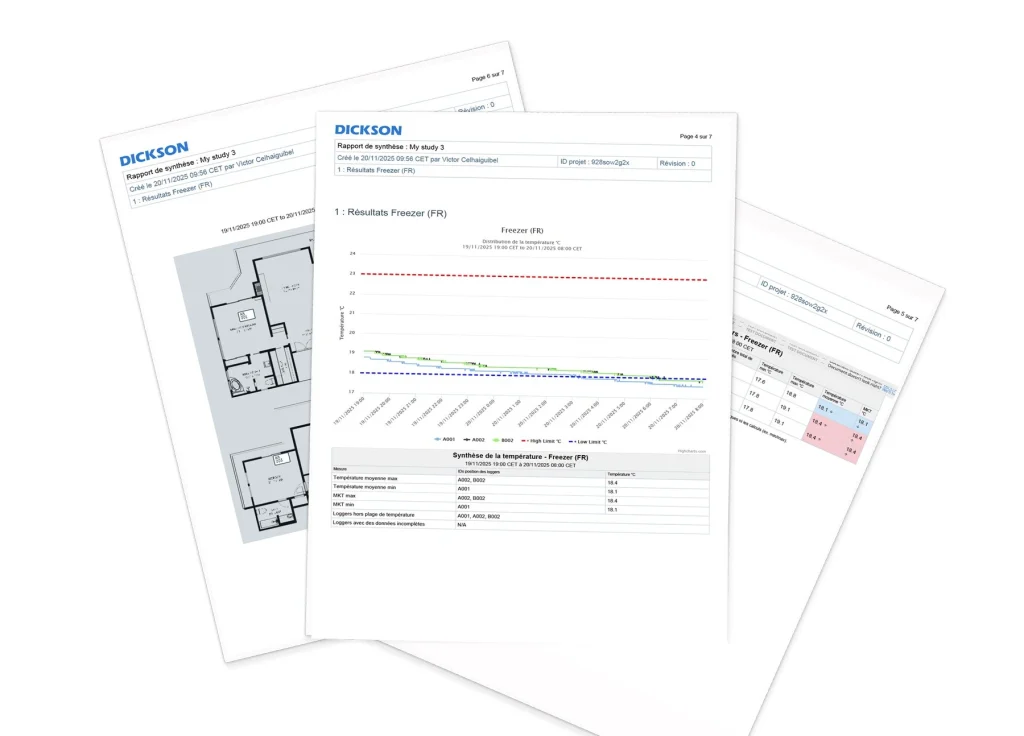
How to Place Data Loggers for Mapping Studies and 3 Ways Dickson Can Help
When it comes to temperature mapping, these two questions create the most confusion: how many loggers do I need, and where exactly should they go?…
How Compounding Pharmacies Can Build a Defensible Differential Pressure Monitoring Program
For years, differential pressure sat in the background of compounding pharmacy monitoring programs — tracked less consistently than temperature and humidity, and enforced less rigorously….
What to Look for in a GxP Metrology Partner for Pharmaceutical Manufacturing
In pharmaceutical manufacturing, there are moments that reveal whether your monitoring vendor is also a true GxP metrology partner. A temperature sensor found out of…

4 Features That Set the Cobalt X Data Logger Apart in Multi-Environment Facility Monitoring
Regulated facilities aren’t simple environments. A single floor might contain ultra-low temperature freezers, CO₂ incubators, a cleanroom, and a cold storage room with different temperature…
Ready to chat?
Talk To A Specialist
Our trained team of professionals is ready to help you through the compliance process from start to finish. Reach out today to start the conversation. Call (630) 563-4209 or send us a message.